
Overview
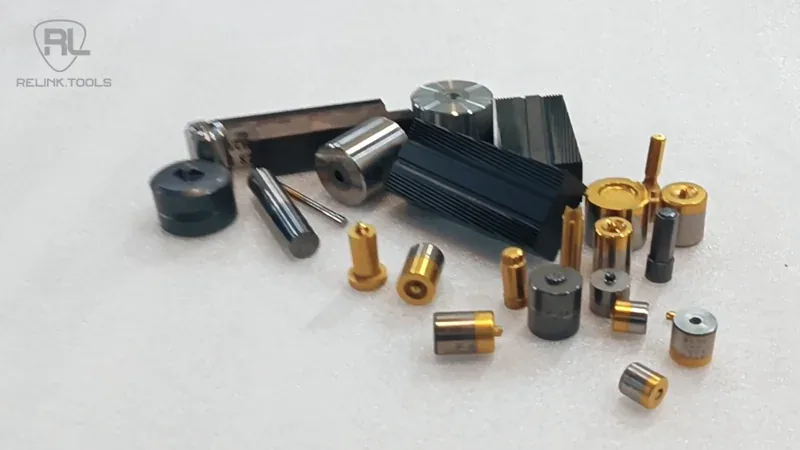
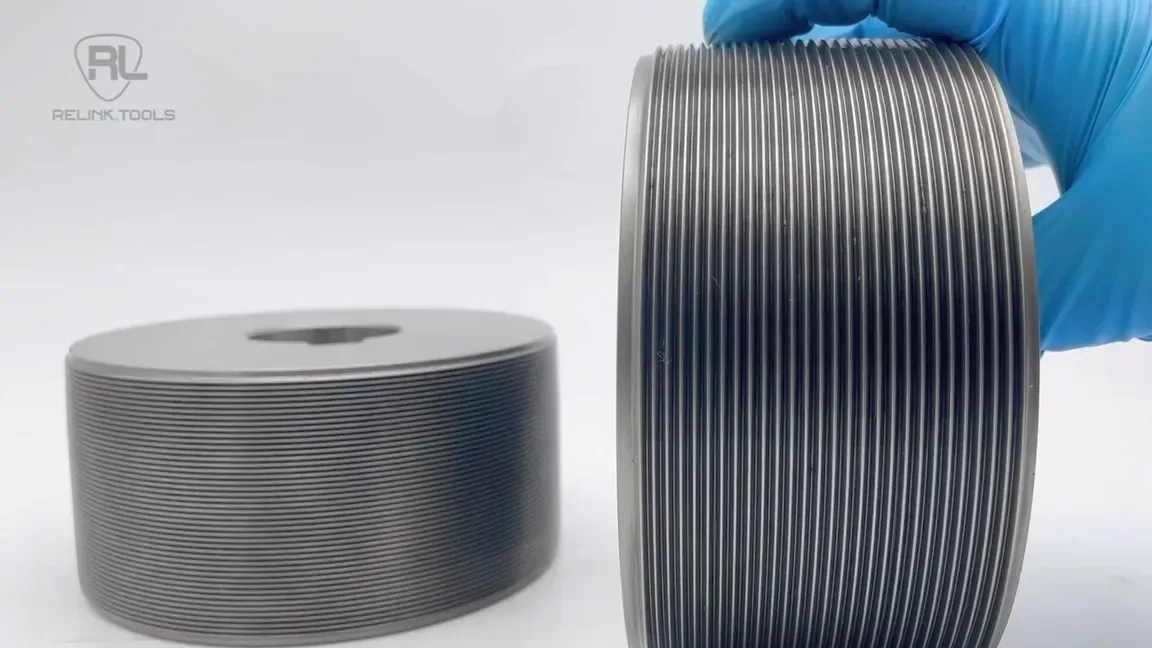
Fastener tooling is two groups of tools: the cold heading tooling that forms the head and shank — punches, dies, trimming dies, knockout pins and extrusion dies — and the thread rolling dies that put the thread on afterwards, flat or cylindrical. Both groups are made to the part and to the machine.
Relink.Tools supplies both for general-purpose fasteners — bolts, screws, nuts, pins and rivets — made to your machine model, your part drawing or a worn sample, with a full-dimension inspection report on every delivery. Heading tools and rolling dies for the same part can go on one order.
If you draw your own wire
Plants that draw their own heading wire can add the drawing dies to the same enquiry. We normally suggest nano-coated dies for the sizes you draw every day and tungsten carbide dies for short runs and trial sizes. Send the rod size, the finished wire size and the number of passes.
For what each stage of a fastener plant needs, see Fastener manufacturing: tooling by stage.
What we supply
| Tool | Where it works | Supplied as | Details |
|---|---|---|---|
| Heading punches | Each station of the header | Carbide or tool steel | Cold header tooling |
| Heading dies | Each station of the header | Carbide insert in a steel case, or tool steel | Cold header tooling |
| Trimming dies | Hex and other non-round heads | Carbide insert or tool steel | Cold header tooling |
| Knockout pins | Eject the part from the die | To drawing | Cold header tooling |
| Extrusion dies | Reduced shank sections | Carbide insert or tool steel | Cold header tooling |
| Flat thread rolling dies | Screws and bolts rolled in volume | Matched pairs, to the machine model | Thread rolling dies |
| Cylindrical thread rolling dies | Larger, longer or closer-tolerance threads, threaded rod, splines and knurls | Sets of two or three, tool steel or carbide | Thread rolling dies |
| Wire drawing dies | Heading wire drawn in your plant | Nano-coated, carbide or PCD | Wire drawing dies |
Carbide goes where the tool wears; tool steel where it takes the shock. One set can mix the two, station by station.
Machines we tool for
Cold headers and part formers
JERN YAO · CHUN ZU · National · Hyodong · Nedschroef · Sacma · Hatebur
Common machine model numbers covered: 104 · 105 · 106 · 134 · 135 · 136 · 164 · 165 · 166 · 204 · 205 · 206 · 254 · 255 · 256 · 276 · 305.
Thread rolling machines
Flat and cylindrical dies are made to the machine model. Give us the model, and the die dimensions if you have them.
Machine not listed? Heading tooling is made to the die-case dimensions of the machine, so send the case dimensions or a worn sample and we will match it.
The machine and brand names above identify compatibility only. Relink.Tools supplies tooling, not the machines.
FAQ
Can I order heading tooling and thread rolling dies together?
Yes. Send the part drawing and both machine models, and one quote covers the heading stations and the rolling dies for that part.
Which cold headers do you supply tooling for?
JERN YAO, CHUN ZU, National, Hyodong, Nedschroef, Sacma and Hatebur, with the common model numbers listed above. For other machines, send the die-case dimensions or a worn sample.
What do you need from me to quote?
For heading tooling: the machine model, the part drawing or a worn tool with its main dimensions, and which stations. For rolling dies: the thread specification, the machine model, and flat or cylindrical. A photo of the worn tool helps.
Do you also supply drawing dies for the heading wire?
Yes. Add the rod size, the finished wire size and the number of passes to the enquiry, and we quote the drawing dies with the heading and rolling tooling.
What is the lead time?
Usually about 15 days, confirmed by item and quantity when we quote.
Request a Quote
Get In Touch QuicklySend us your machine model or drawing, the wire or material, and the quantity. We will prepare a quotation.